
01AW / TOOL
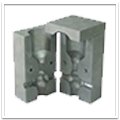
Graphite Mould
Graphite Mould
The connection Mould is designed to last for an average of 60 to 100 connections.
Read MoreField Equipment / 01
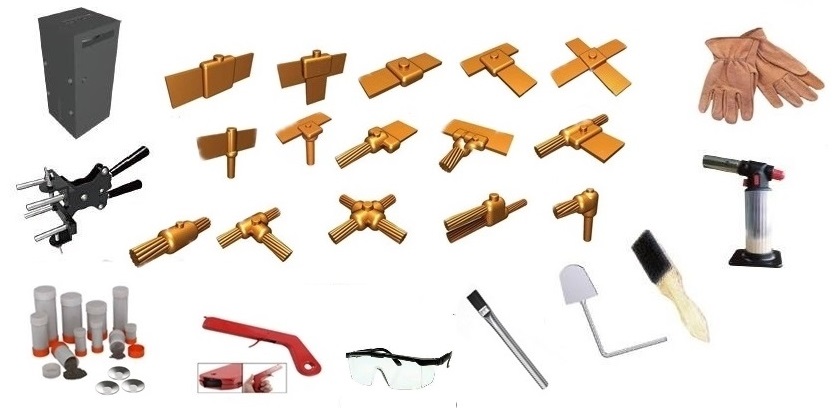
Every dependable field connection begins with a complete, well-prepared system. Explore the mould, consumables, handling tools, cleaning equipment and safety accessories used throughout the process.
Complete Range / 02
We manufacturer, supply and export Exothermic Welding Mould and Its Accessories across World.
The connection Mould is designed to last for an average of 60 to 100 connections.
Read More
Steel discs acts timing device to allow the welding powder to heat to proper temperature.
Read More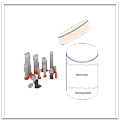
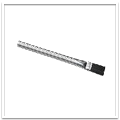
Soft Brush – Clean Mould Weld Cavity because its shape is very sensitive
Read More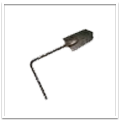
It is used to remove the metal Scrap from Mould after the Welding Process is done.
Read More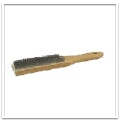
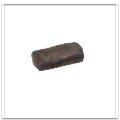
Sealing Compound is used to fill the gap on the mould where the conductor is passing.
Read More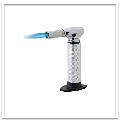
There is a need for propane torch to dry out the inside of the mould thoroughly on both sides.
Read MoreFlame Torch: There is a need for propane torch to dry out the inside of the mould thoroughly on both sides.
Read MoreTechnical Reference / 03
Select an accessory to review its purpose, working guidance, features and recommended usage. Each “Read More” link above opens the matching reference below.
Precision ToolingGraphite MouldDesigned for precise and reliable exothermic weld connections.
We Manufactured Graphite Mould which ensure optimum results. Each Graphite Weld Mould is designed to give precise and reliable results. Amiable Impex used the finest quality of Weld Mould that can withstand continuous heat-cooling cycles. The connection mould is designed to last for an average of 60 to 100 connections. This will vary according to the care given the mould during use.
Universal HandlingMould Handle ClampHandles and securely clamps the mould halves together.Handle clamps provide a means of both handling the mold, and also of clamping the mold halves together. For most connections involving lugs, cable or rectangular bus, Exothermic handle clamps are used. These will fit 90% of all standard exothermic molds.
Normally we recommend One Handle for every two moulds. These are manufactured by the professionals using high quality raw material. These Mold Handle Clamp conform their adherence with the industry standards.
Reaction ControlSteel Metal DiskA timing device that contains the reaction until it is ready to weld.Steel discs acts timing device to allow the welding powder to heat to proper temperature. Steel Disk is designed to contain the exothermic reaction to the upper crucible of a mold until the reaction is complete and ready to weld. One Metal is must for every shot.
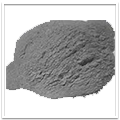
Weld MaterialExothermic Weld PowderReliably and consistently performing weld metal.We offer Exothermic Weld Powder that is the most reliable and consistently-performing weld metal. Quality validation steps are taken for every lot we produce. Upon final acceptance, our weld metal is specially packaged in moisture-resistant plastic cartridges with special closure caps. Then the cartridges and required metal discs are packaged in moisture-resistant boxes.
Standards Size Packing available are – 15 Grams, 25 Grams, 45 Grams, 65 Grams, 90 Grams, 115 Grams, 150 Grams, 200 Grams, 250 Grams. Moisture Free Packing in Foil.
Starting MaterialIgnite PowderAlso known as Starting Powder, used to initiate the reaction.Ignite Powder is also known as Starting Powder. Sprinkle little Starting Powder on the Mold followed by the Exothermic Weld powder and again sprinkle it little on the Top Side of Mould. Than Ignite starting powder with a spark gun. This results in exothermic reaction and the weld powder melts to molten copper alloy. The molten copper alloy melts the retaining disc and flows into the weld cavity where it partially melts the conductors.
Ignite Powder of 2-4 grams is sufficient for this Process.
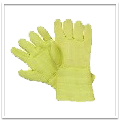
Operator SafetyHand GlovesRequired protection for high-temperature field work.Gloves is required for safety purpose as the Exothermic Weld Powder melts at more than 1400 degree Celsius. We recommend a Pair of Gloves for Every 150 to 200 Joints.
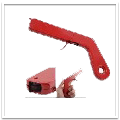
Safe IgnitionFlint GunDesigned for safe and convenient starting-powder ignition.Flint Gun is designed with the advantages of safety and convenience. It is used to ignite Starting Powder in orderto result in exothermic reaction. We recommend one Flint Gun for every 80 to 100 Shots.
Mould CareBrush (Soft and Hard)Two brush types for sensitive cavities and other mould sections.Two Brush is Required:
Post-Weld CleaningSlag Removal ToolRemoves metal scrap from the mould after welding.It is used to remove the metal Scrap from Mould after the Welding Process is done. We recommend One Slag Tool for Every 200 Joints.
Conductor PreparationFile CardUsed to clean the objects before welding.It is used to clean the objects to be welded. We recommend One Slag Tool for Every 100 Joints.
Leakage ControlSealing CompoundFills the mould gap around the passing conductor.Sealing Compound is used to fill the gap on the mould where the conductor is passing We recommend 1 Kg Sealing Compound for Every 100 Joints.
Moisture RemovalFlame TorchDries the graphite mould thoroughly before welding.Graphite absorbs moisture from weather. So there is a need for propane torch to dry out the inside of the mould thoroughly on both sides, therefore heating the mold to approximately 250 degrees Fahrenheit We recommend using one Flame torch for Every 200 Joint and than use the refiling.
Share your project requirements with our team for product guidance, technical support and a prompt response.
Amiable Impex