STEP – 1
Always wear protective safety glasses and gloves while working with exothermic welding products.
Overview / 01
An Exothermic Weld has higher mechanical strength than other forms of weld, and excellent corrosion resistance.
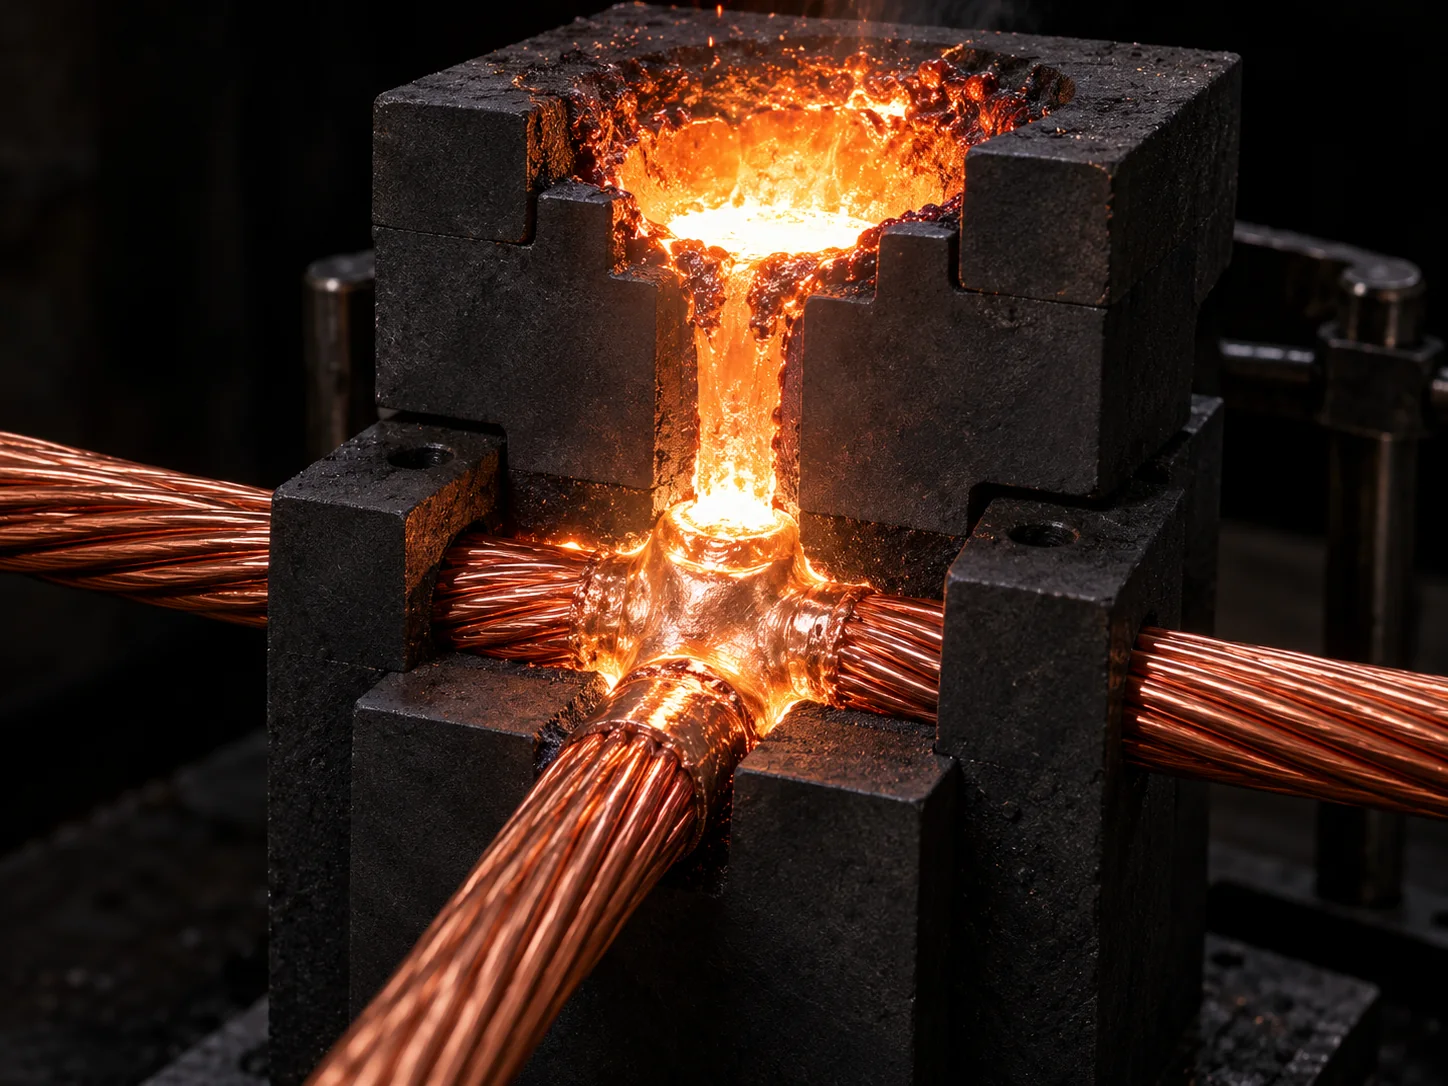
Exothermic weld process for joining two electrical conductors that employs superheated copper alloy to permanently join the conductors. The process employs an exothermic reaction of a copper thermite composition to heat the copper, and requires no external source of heat or current. The chemical reaction that produces the heat is an aluminothermic reaction between aluminum powder and a metal oxide.
The reaction reaches very high temperatures, depending on the metal oxide used. The reactants are usually supplied in the form of powders, with the reaction triggered using a spark from a flint lighter. The activation energy for this reaction is very high however, and initiation requires either the use of a “booster” material such as powdered magnesium metal or a very hot flame source. The aluminum oxide slag that it produces is discarded.
Graphite Crucible Mould / 02
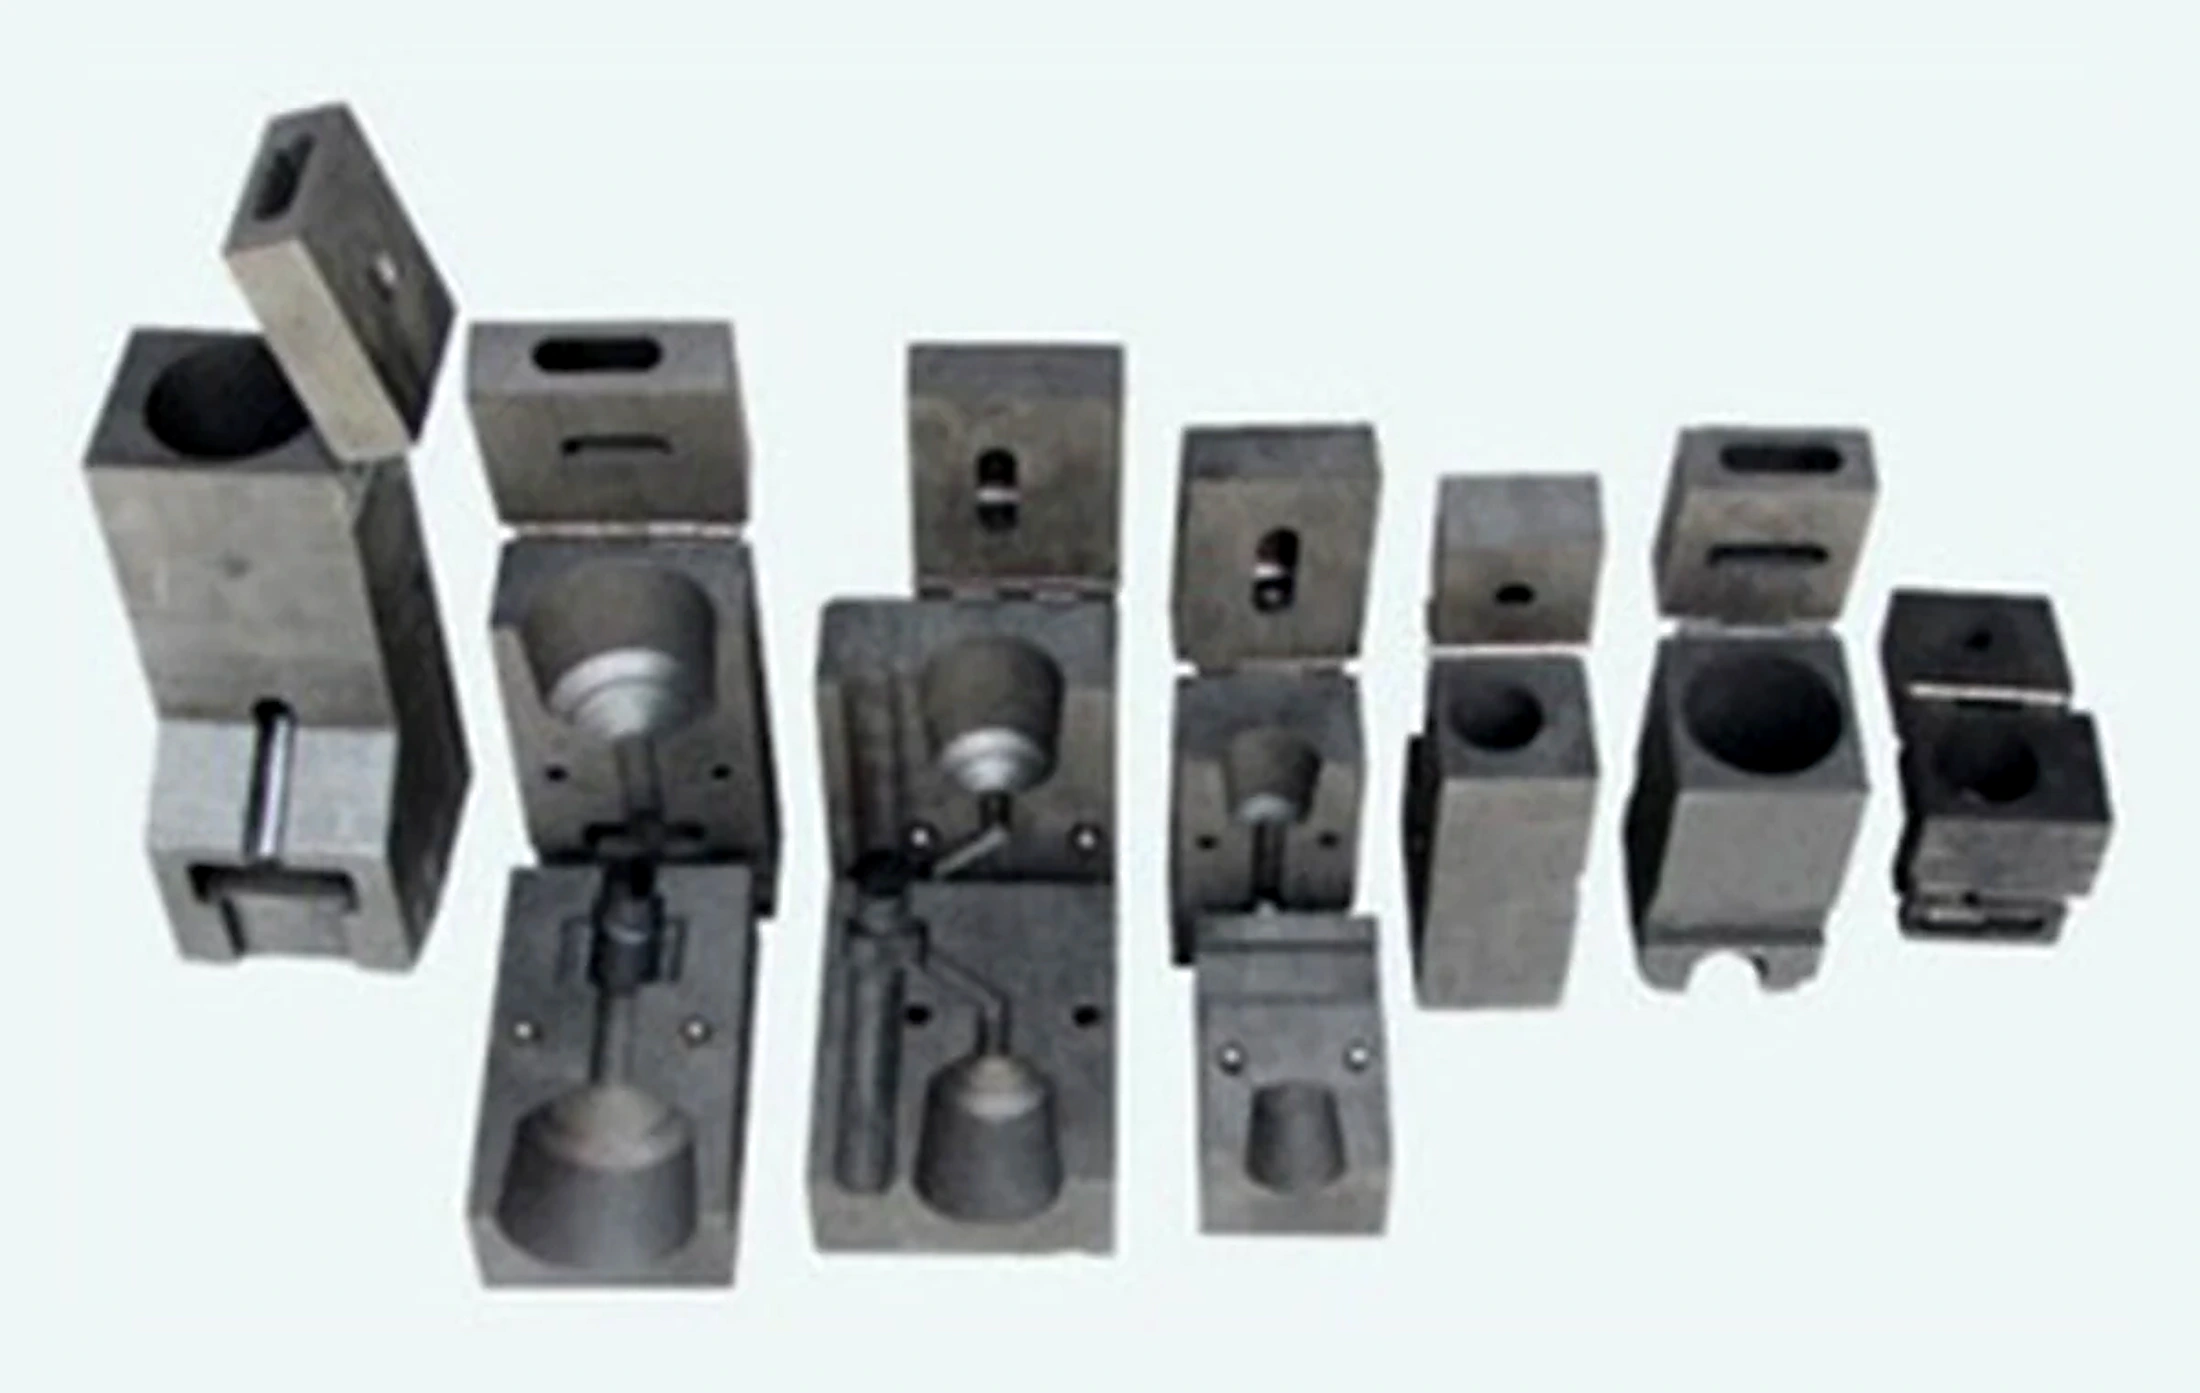
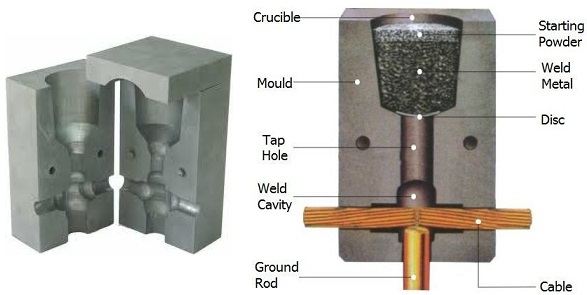
When welding copper conductors, the process employs a semi-permanent graphite crucible mould, in which the molten copper, produced by the reaction, flows through the mould and over and around the conductors to be welded, forming an electrically conductive weld between them. When the copper cools, the mould is either broken off or left in place. Alternatively, hand-held graphite crucibles can be used. The advantages of these crucibles include portability, lower cost and flexibility, especially in field applications.
The weld formed has higher mechanical strength than other forms of weld, and excellent corrosion resistance. It is also highly stable when subject to repeated short-circuit pulses, and does not suffer from increased electrical resistance over the lifetime of the installation. However, the process is costly relative to other welding processes, requires a supply of replaceable moulds, suffers from a lack of repeatability, and can be impeded by wet conditions or bad weather.
In Detail / 03
Exothermic weld is a joining technique used to create a permanent connection between two metallic components. It involves a chemical reaction that generates heat, known as an exothermic reaction. This process is particularly noted for the durability of the bond produced and for preserving good electrical conductivity between the joined components.
Creating a bond by exothermic weld typically involves heat created by a chemical reaction between some type of heavy metal oxide and a reducing agent. For example, iron oxide is a commonly used metal oxide and aluminum is a common reducing agent. These reactants produce heat extremely rapidly when ignited, thereby achieving the high temperatures needed for welding.
Such heating is generally initiated once the parts to be joined are fitted together in a mold which contains the materials and the reaction as it takes place. Filler metal in liquid form is produced by this reaction and mixes with melted metal from the parts being joined to form a bond shaped by the mold. Molds used in exothermic weld may be made of graphite, ceramic, or other appropriate materials.
Exothermic weld connects cables, ground rods, terminals and structures; the resulting molecular bond produces a permanent connection that won’t loosen or corrode over the lifetime of the installation. You should use exothermically welded connections when: you require long life/permanent connections; you expect high current faults; or corrosive conditions exist.
The equipment required to make exothermic connections is lightweight, portable and does not require outside power. The resulting bond is a permanent joining of metallic parts that form an electrically conductive path. This will ensure electrical continuity and the capacity to conduct any potential current safely.
These permanent connections will carry as much, or more, current as the conductor. These connections eliminate bimetallic corrosion at the point of the weld. All strands of the conductor will equally share the current load.
Exothermic weld system from provides precision engineered molds for optimal results. Permanent molecular bonding is the preferred method for making copper to copper and copper to steel electrical connections. It is a connection using a high-temperature exothermic reaction that does not require an external heat or power source. Its performance is superior to all existing surface to surface connectors. Features include simplicity, corrosion resistance, extended shelf life, high conductivity, portability, ease of use, and it requires no external heat or power source.
Process for Exothermic Weld is as follows:
Follow the given Steps to do Exothermic Welding :
Always wear protective safety glasses and gloves while working with exothermic welding products.
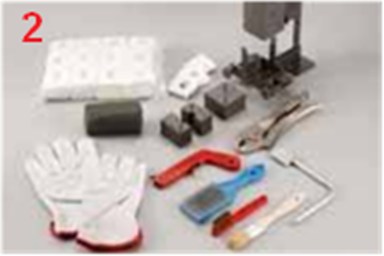
Gather all the proper material and equipment/accessories for the type of connection you are making. The typical Weld system requires a graphite mold, handle clamp, welding material, natural bristle brush for mold cleaning, wire brush for cleaning/preparing conductors, flint igniter, and propane torch. Check to ensure the graphite mold is not worn or broken, which could cause leakage of molten weld metal.
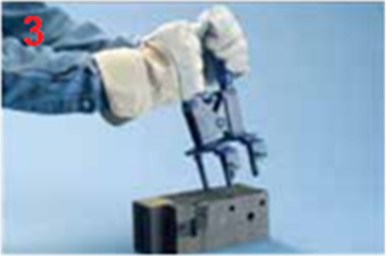
Slide the handle clamp into the pre-drilled holes with the proper orientation for the thumbscrews.
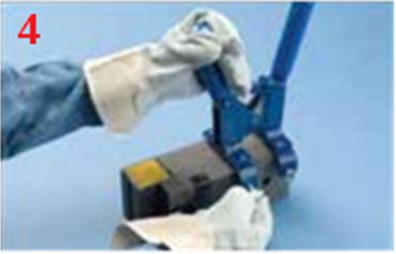
Tighten the clamp thumbscrews onto the mould.
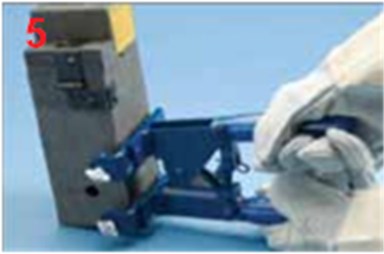
Close the grips to tightly lock the mold. Make adjustments to tighten/loosen the handle clamp.
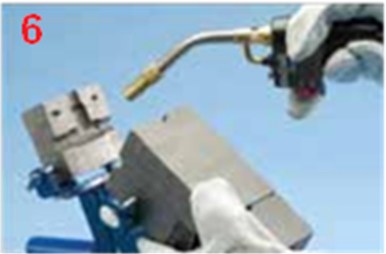
The material to be welded (cable, rod, tape) must be clean and dry using the brush included in the set of accessories. Thus the oxide layer and superficial impurity is eliminated. Given that the graphite mould also absorbs moisture, this should be removed by preheating with a gas welding torch to avoid a porous welding. After the first welding is done, it is not necessary to re-heat the mould if the next welding is done within 15 minutes as it conserves the previously generated heat.
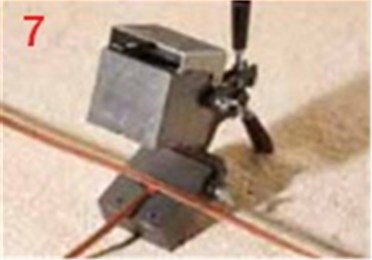
Place the conductors in the mould and close the handle clamps to avoid material leakages during the reaction.
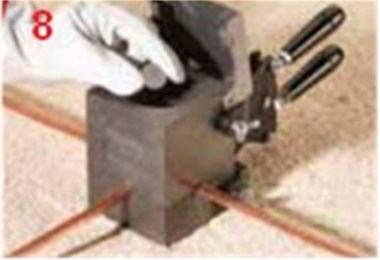
Obstruct the tap hole with the metallic disk.
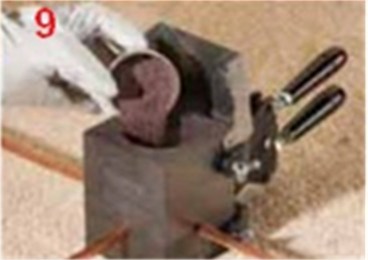
Empty the contents of the welding mixture package.
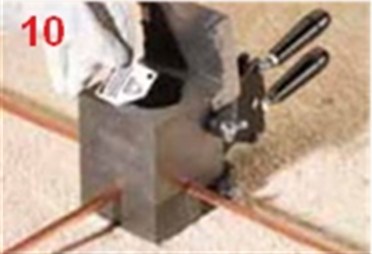
Empty 50% of the starting powder above Exothermic Weld Powder (Don’t Mix, just scatter) and than Close the Mould Mouth and than the rest 50% Starting Powder, Sprinkle it on the Mould Mouth nearby the small hole given on the top of the Mould Mouth.
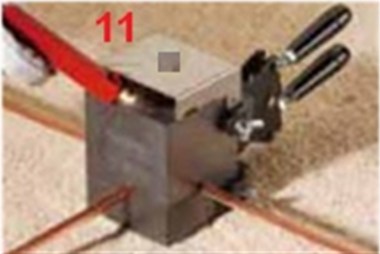
Ignite the starting powder extended on the top/side of the mould using the flint Igniter.
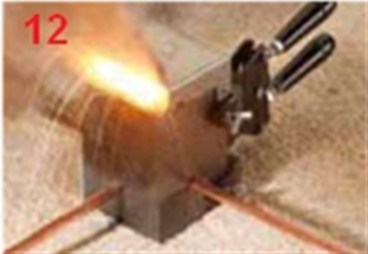
Once started, the reaction will take 3-4 seconds during which it is recommended to stand clear of the mould.
After at least 2 minutes of the bonding, open the mould by undoing the handle grip. Remove the mould from the joint and clean the joint for any slag. Once open, clean the slag sticking to the mould with the relevant tool and clean the cavities. The mould will be ready now to use again without having to re-heat it as it is already warm.